EN
 CN
 fr
 es
 ar
 ru
 de
 pt
 tr
 vi
 it
 ja
 ko
 hi

How Manganese Carbonate Is Used in Glazes and Ceramic Coatings
Artisans utilized manganese-derived browns and purples in Tang Dynasty ceramics centuries ago. Modern engineers now incorporate these exact same compounds into high-precision industrial coatings. The fundamental chemistry remains unchanged. However, the production scale and quality requirements are entirely different. Manganese carbonate acts as a highly functional design tool. It provides ceramicists and engineers with predictable and repeatable color effects. It also enables highly specific surface textures.
This article serves as a comprehensive field guide for studio formulators, industrial coating engineers, and procurement teams. You will learn exactly how manganese carbonate in glazes behaves during firing. We will explain how manganese carbonate ceramic coatings achieve specific variables. You will also learn how to specify the optimal bulk grade for your facility. We supply these materials with deep formulation-level technical knowledge to ensure a strong economic return on investment (ROI) for your production lines.

Why Manganese Carbonate Is the Preferred Glaze Ingredient
Formulators frequently ask why they should select manganese carbonate (MnCO₃) instead of manganese dioxide (MnO₂) or manganese oxide (MnO). The answer lies primarily in the decomposition advantage.
MnCO₃ decomposes cleanly at approximately >200 °C. The compound releases carbon dioxide (CO₂) and leaves behind highly reactive MnO. This "in-situ reduction" moment makes it vastly superior to pre-oxidized forms. The nascent MnO integrates into the molten glaze matrix exceptionally homogeneously. Conversely, MnO₂ particles require much higher temperatures to integrate. They also carry residual oxygen that routinely causes micro-bubbling defects. Formulators immediately appreciate this kinetic advantage. MnCO₃ meets the glaze melt at the exact right oxidation state.
Particle size and dispersion matter just as much as chemical purity. Fine-ground MnCO₃ with a D50 under 10 µm yields vastly smoother color development than coarser grades. Industrial spray coatings and roller-applied ceramic tile glazes rely completely on this uniformity. Particle size directly dictates color batch repeatability. Procurement engineers must always request particle size distribution (PSD) data alongside standard purity specifications.
Comparison Snapshot: Glaze Contexts
| Feature | Manganese Carbonate (MnCO₃) | Manganese Dioxide (MnO₂) |
|---|---|---|
| Decomposition Temp | >200 °C | Stable up to ~550 °C |
| Glaze Integration | Homogeneous via in-situ reduction | Particulate; requires higher heat |
| Bubble Risk | Low (CO₂ escapes early) | High (Residual oxygen release) |
| Overall Value | Best balance of consistency and cost | Less ideal for standard firing ranges |
MnCO₃ clearly offers the best balance of color consistency, processing ease, and operational cost for standard ceramic firing ranges between 1000 °C and 1300 °C.
The Color Chemistry: What Manganese Carbonate Does Inside a Fired Glaze
Manganese carbonate creates remarkably distinct outcomes inside a fired glaze. The kiln atmosphere acts as a primary control variable. Oxidation firing in electric kilns keeps the manganese in the Mn³⁺ or Mn⁴⁺ state. This state reliably produces warm browns, ambers, and muted purples. Reduction firing in gas or wood kilns partially reduces the manganese to Mn²⁺. This specific reduction yields cooler, greyer tones. The color can even shift toward dark charcoal and slate. You can view this as a programmable outcome from a single raw ingredient. Industrial tunnel kilns and roller hearth kilns typically run oxidizing atmospheres for commercial tile and sanitaryware.
The base chemistry of the glaze also dictates the final appearance.
- High-calcium glazes: Manganese shifts toward warmer browns because calcium stabilizes the Mn³⁺ ions.
- High-alkali glazes: Sodium and potassium push the color toward vibrant violet. This mechanism creates classic manganese purple glazes.
- Zinc-containing glazes: Zinc fundamentally suppresses manganese color development. Formulators must avoid this common mistake.
- Boron-fluxed glazes: Low-fire formulations utilize MnCO₃ well between 1000 °C and 1100 °C to achieve warm chocolate tones.
Concentration levels dictate everything from subtle tints to aggressive coloration. Formulators use a 0.5% to 1% addition to create a barely perceptible warm tint that softens overly bright whites. An addition of 2% to 4% provides reliable medium brown development. This represents the standard range for production tile glazes. Additions of 5% to 8% create deep brown to near-black colors. However, the risk of crawling and pinholing increases significantly above 6%. Additions above 8% create specialized matte and textured effects. Technicians typically combine these high levels with rutile or iron oxide.
Manganese also alters surface textures beyond basic color. High loadings promote distinct matte and crystalline surface textures. This occurs due to partial devitrification during cooling. Artisan stoneware producers deliberately use this property to create tactile, non-reflective finishes. Industrial manufacturers apply these manganese-modified matte glazes to produce highly effective anti-slip floor tiles.
Application-by-Application Breakdown
Ceramic Floor and Wall Tile Manufacturing
This sector represents the largest volume application globally. Manufacturers use MnCO₃ in body stains, engobe layers, and surface glazes. The compound plays a critical role in achieving the earthy, natural-stone aesthetics that dominate architectural trends. A typical surface glaze utilizes 2% to 5% by dry weight. Body stains require 0.5% to 2%. The material offers flawless compatibility with spray glazing, waterfall application, and dry granule decoration techniques.
Sanitaryware (Vitreous China)
Factories use MnCO₃ in underglaze colorants and body formulations for basins, toilets, and bathtubs. These continuous processes demand exceptional chemical purity to avoid color inconsistency. Strict particle size control remains absolutely critical. Inconsistent sizing causes distinct color streaking in spray-applied glazes on complex three-dimensional forms. Purity requirements strictly demand ≥44% manganese content. Suppliers must maintain heavy metals at trace parts-per-million levels to ensure global compliance.
Porcelain Tableware and Decorative Ceramics
Formulators rely on MnCO₃ for underglaze pigments and in-glaze stains. They achieve excellent brown, purple-brown, and grey tones. Technicians often combine it with cobalt for blue-brown blends or iron oxide for deeper earthy hues. Consumer products face strict EU Regulation (EC) No 1935/2004 and FDA requirements. Strict heavy metal release limits apply stringently to all food-contact ceramics.
Technical and Industrial Ceramics
Engineers utilize MnCO₃ as a sintering aid and performance colorant. Manufacturers use it within alumina-based technical ceramics. They also apply it in specialized ceramic coatings for electronic substrates. The MnO derived from MnCO₃ strongly aids densification at lower temperatures. An exciting emerging application involves manganese-doped ceramic coatings for thermal barrier applications in the aerospace and energy sectors.
Roof Tiles and Exterior Architectural Ceramics
Architectural ceramics feature prominent earthy brown and terracotta tones. MnCO₃ achieves these exact colors without the inherent variability found in natural clay pigments. Manganese-based colors demonstrate exceptional lightfastness. This UV stability represents a non-negotiable performance requirement for exterior applications. Manganese-modified glazes also show superior resistance to acid rain and harsh freeze-thaw cycling.
Studio Pottery and Artisan Ceramics
This smaller but influential buyer segment remains highly quality-conscious. Independent artists specify purity and particle size very explicitly. Studio glaze innovations frequently become industrialized a decade later. Therefore, the manganese carbonate pottery glaze remains a vital creative and industrial benchmark.
Formulation Best Practices: Getting Consistent Results
Formulators must follow strict best practices to guarantee consistent results with manganese carbonate.
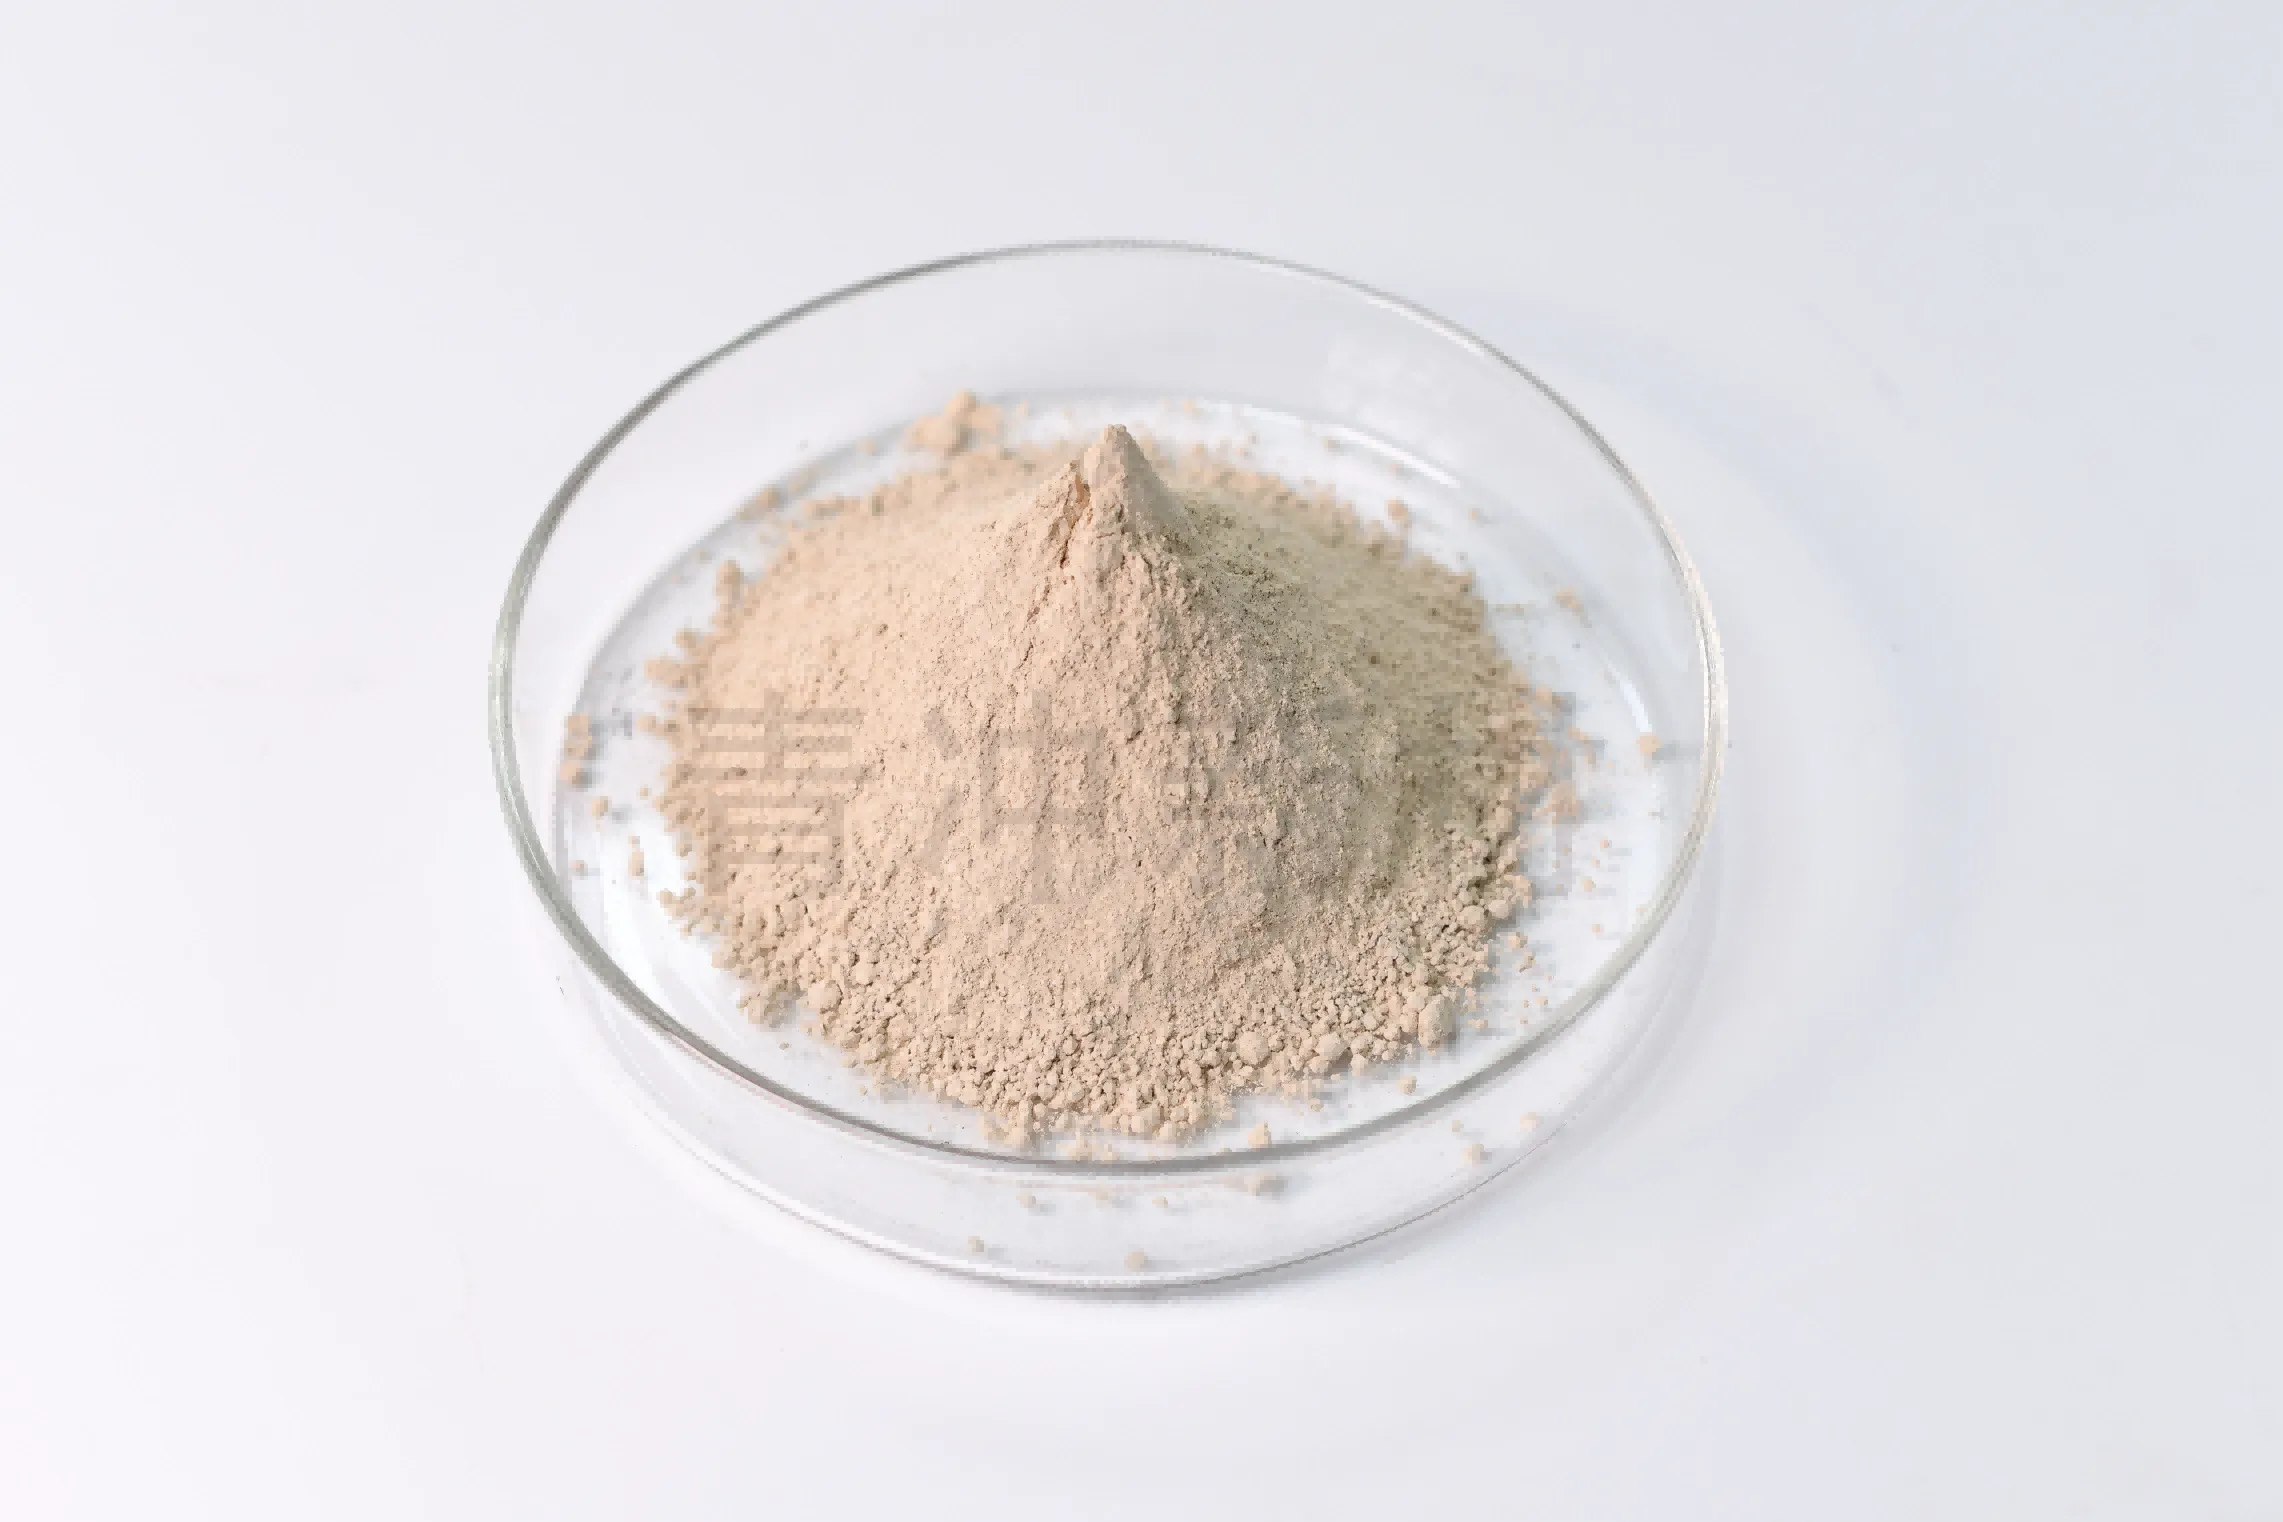
Milling and dispersion protocols require careful execution. You must always ball-mill the MnCO₃ with the entire base glaze batch. Dry mixing alone will inevitably cause agglomeration and color spotting. You should target specific gravity and Baumé parameters carefully before application. MnCO₃ slightly increases the overall slurry density. Viscosity control remains highly critical for spray applications. We strongly recommend Seeger or Ford cup testing immediately after the manganese addition.
Firing curve considerations directly impact your final surface quality. The primary CO₂ release from MnCO₃ occurs greater than 200 °C. You must ensure adequate kiln ventilation during this phase to prevent glaze crawling. Soaking at peak temperatures improves color development and surface smoothness. Peak temperatures generally sit at 1220 °C to 1280 °C for stoneware and 1050 °C to 1150 °C for earthenware. A slow cooling phase through 573 °C (quartz inversion) and the 550 °C to 400 °C range significantly improves manganese color richness.
Formulators must accurately diagnose common root-cause problems.
- Pinholing: This usually stems from MnCO₃ additions above 5% without an adjusted flux balance. You must reduce the colorant or add a low-viscosity flux.
- Color Batch Variation: This almost always indicates a particle size or supplier-grade inconsistency. You must strictly enforce PSD requirements with your supplier.
- Crawling: This happens when CO₂ off-gassing becomes trapped under a melting glaze skin. You must raise the early-stage temperature ramp to allow full degassing.
- Unexpected Matte Finishes: Manganese levels above 4% actively promote devitrification. You must adjust your formula downward if a high-gloss finish is required.
Combination colorants vastly expand the design palette. Mixing MnCO₃ with iron oxide creates deep rustic browns and heavy blacks. Mixing it with cobalt oxide produces striking violet to purple-grey tones for high-end porcelain. Mixing it with rutile creates beautifully textured, variegated finishes. You must carefully note chemical interactions before proceeding. Cobalt amplifies manganese purple, while iron strongly suppresses it. You must test-fire all combinations thoroughly before initiating production scale-up.
Conclusion
Manganese carbonate is far more than a simple colorant. It serves as a chemically active glaze ingredient whose final behavior is determined entirely by firing atmosphere, base chemistry, particle size, and concentration. Floor tile, sanitaryware, porcelain, technical ceramics, and exterior cladding all rely on this precise compound.
However, engineers specify the material completely differently for each application. A consistent raw grade guarantees consistent results at the kiln.
Share your specific glaze firing temperature, application method, and target visual effect with us today. Our technical team will recommend the exact right MnCO₃ grade to maximize your B2B conversion and ROI.
You can follow the links on our website to review our comprehensive MnCO₃ product data sheets. We leverage decades of industry experience, serve many global customers, and maintain rigorous certifications to ensure your continuous operational success.
FAQs
1. Why should I use manganese carbonate instead of manganese dioxide in a ceramic glaze?
Manganese carbonate decomposes cleanly at lower temperatures (>200 °C) and disperses much more evenly into the glaze melt. It also avoids the micro-bubbling issues associated with the residual oxygen release from manganese dioxide.
2. Can adding too much manganese carbonate cause my glaze to pinhole or crawl?
Yes. Adding concentrations above 5% frequently causes pinholing if you do not adjust your flux balance correctly. Crawling also occurs if your early-stage firing ramp traps the escaping carbon dioxide gas beneath the melting glaze surface.
3. How does the kiln atmosphere change the color of a manganese glaze?
Oxidation firing in an electric kiln keeps the manganese stable, producing warm browns, ambers, and purples. Reduction firing in a gas or wood kiln reduces the manganese state, which shifts the final color toward cooler greys, charcoals, and slate tones.
4. Is manganese carbonate safe to use in glazes for food-contact tableware?
Yes, it is entirely safe if you source a high-purity grade with strictly controlled heavy metal limits. Manufacturers must ensure their final fired products comply with specific FDA and EU leaching regulations.
5. What is the optimal particle size for a manganese glaze colorant?
A fine-ground specification with a D50 particle size under 10 µm is ideal for surface glazes. This fine distribution ensures smooth, consistent color development without speckling or batch-to-batch variation.